
Electroplating Learn.
Everything you need to know about electroplating but were afraid to ask. We break down complex coating processes into plain English so you can talk intelligently with suppliers, write better specifications, and avoid expensive mistakes. Think of this as electroplating school without the boring lectures or pop quizzes. Real knowledge from 30 years in the tanks.
Testing Methods
Advanced TopicsQuality Verification
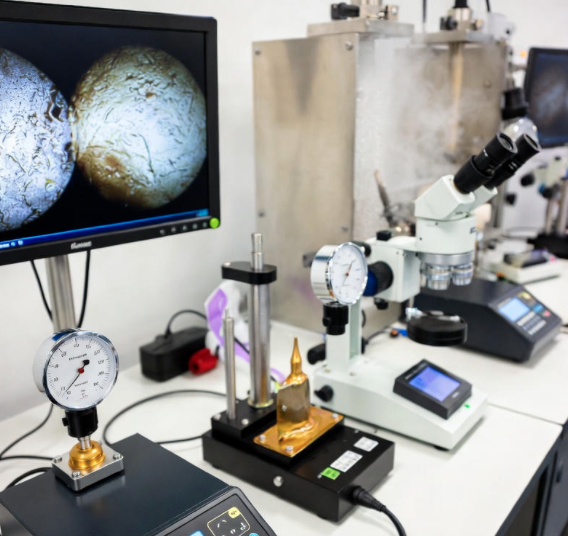
Testing Programs: Verification ensures specifications are met.
Electroplating quality depends on properties invisible to naked eye. Appearance inspection catches obvious defects but missing thickness, poor adhesion, or inadequate corrosion resistance slip through visual screening. Testing verifies coating meets specifications through objective measurements. Different properties require different test methods. Thickness measurement most common. Adhesion testing validates bond strength. Salt spray evaluates corrosion resistance. Hardness testing confirms mechanical properties. Porosity tests reveal coating integrity. Each test serves specific purpose answering questions about coating performance. Comprehensive quality programs combine multiple tests ensuring all critical properties meet requirements before shipping parts to customers.
Thickness Measurement
Coating thickness represents most frequently tested property because specifications usually define minimum and maximum limits. Multiple measurement technologies exist each with advantages. X-ray fluorescence (XRF) non-destructively measures thickness and composition simultaneously. Magnetic gauges work on ferrous substrates using magnetic attraction. Eddy current instruments measure non-magnetic coatings on non-ferrous substrates through electromagnetic induction. Coulometric testing strips coating electrochemically measuring charge required revealing thickness. Microsectioning cuts parts showing cross-section under optical microscope. Each method has accuracy, cost, and application range trade-offs. XRF dominates production testing offering speed, accuracy, and multi-layer capability. Destructive methods provide validation when disputes arise over non-destructive results.
Non-Destructive
XRF testing. Magnetic gauges. Eddy current instruments. Parts remain usable after testing. Fast results. Good for production screening.
Destructive
Coulometric stripping. Microsectioning. Parts destroyed during test. Higher accuracy. Validation and dispute resolution.
Adhesion Testing
Coating adhesion determines whether deposit stays bonded or peels during service. Multiple test methods assess bond strength. Tape test applies adhesive tape then rips off checking for coating removal. Simple but subjective. Bend test flexes plated strips around mandrels watching for cracking or separation. Reveals brittleness and poor adhesion. File test scrapes coating with hardened file evaluating resistance. Heat-quench test thermal shocks parts causing weak bonds failing. Peel test mechanically measures force required separating coating. Most quantitative but requires special sample preparation. Specifications define which tests to perform and acceptance criteria. Running adhesion tests during process qualification and periodically throughout production catches problems before customer rejects.
Tape Test Procedure
Clean coating surface removing contamination. Apply strong adhesive tape firmly pressing out air bubbles. Quickly rip tape off at 90-degree angle. Examine coating for removal or lifting. Good adhesion shows no coating on tape and no damage to deposit. Any removal indicates adhesion problems requiring corrective action before continuing production.
Salt Spray Testing
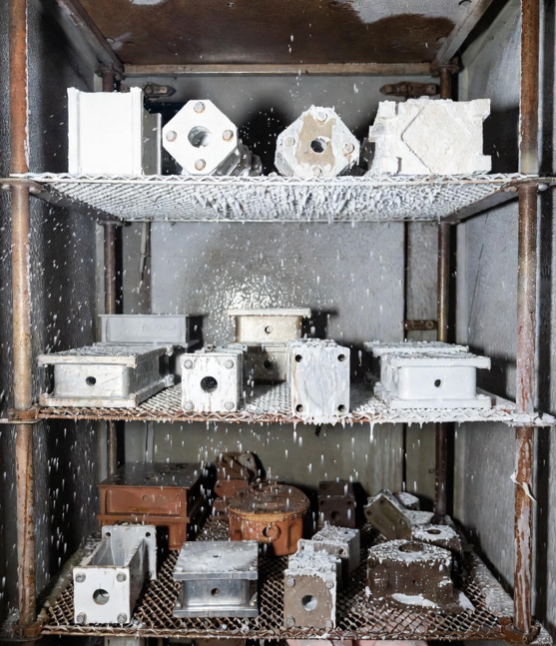
Corrosion Resistance: Salt spray simulates harsh environments.
Salt spray testing (ASTM B117) exposes parts to continuous salt fog simulating accelerated corrosion. Test duration varies from 24 hours to 1000+ hours depending on coating system and specification requirements. Periodic inspection evaluates corrosion appearance. Neutral salt spray uses 5% sodium chloride solution. Accelerated tests like CASS (copper-accelerated acetic acid salt spray) speed corrosion for faster results. Test results correlate loosely with outdoor exposure but don't perfectly predict field performance. Salt spray validates coating system provides specified protection level. Passing 96-hour test doesn't guarantee 10-year service life but failing 24 hours predicts premature failure. Useful quality gate catching obvious coating defects before shipping.
Hardness Testing
Coating hardness indicates wear resistance and mechanical properties. Vickers microhardness testing indents coating with diamond pyramid measuring impression size under microscope. Reported as HV with units like 200 HV typical for bright nickel or 800+ HV for hard chrome. Knoop hardness uses elongated diamond indenter suitable for thin coatings. Rockwell testing works for thick deposits but too coarse for thin films. Sample preparation critically affects results requiring polished cross-section for accurate measurement. Hardness correlates with wear resistance but relationship depends on coating type and application. Measuring hardness validates chemistry and process parameters producing intended properties. Changes indicate chemistry drift requiring correction.
| Test | Property | Method |
|---|---|---|
| XRF | Thickness | X-ray fluorescence |
| Tape Test | Adhesion | Adhesive removal |
| Salt Spray | Corrosion | Accelerated exposure |
| Vickers | Hardness | Microindentation |
Porosity Testing
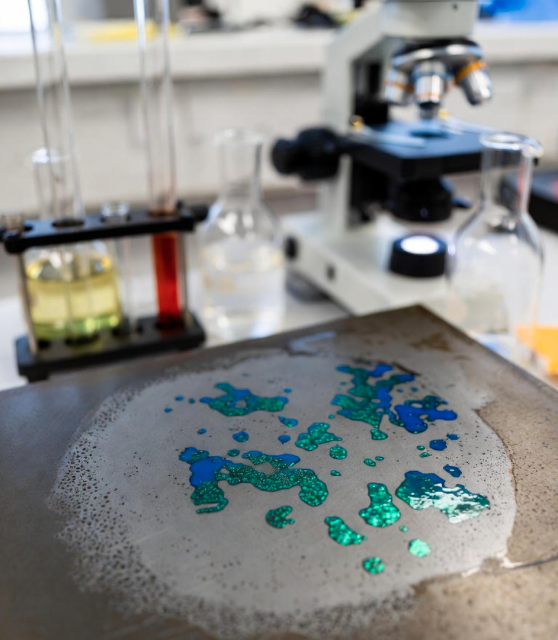
Pore Detection: Identifying coating discontinuities.
Porosity testing reveals pores or discontinuities in coating allowing substrate access. Ferroxyl test detects pores in coatings on steel. Apply reagent forming blue-green spots where iron exposed through pores. Count pores per unit area comparing to specification limits. Electrographic testing uses electrically conductive paper detecting pores through current flow. Pore density indicates coating protective capability with fewer pores providing better protection. Porosity correlates inversely with thickness—thicker coatings have fewer through-pores. Multi-layer systems reduce porosity through offset pore structure between layers. Specifications sometimes limit acceptable pore count especially for corrosion-critical applications. Testing validates process producing sufficiently dense protective coating.
Quality Programs
Effective quality programs combine testing, documentation, and corrective action. First-piece inspection validates setup before production run. In-process testing catches problems during production enabling correction. Final inspection verifies finished parts meet specifications. Test frequency balances confidence against cost. High-volume repetitive work supports statistical sampling. Critical aerospace applications demand 100% testing. Documentation proves compliance when customer audits or disputes arise. Control charts track test results over time revealing trends indicating chemistry drift or process changes. Out-of-specification results trigger root cause investigation and corrective action. Testing without action wastes money. Testing with systematic response prevents defects reaching customers.
Testing Strategy
First-piece verification. In-process monitoring. Final inspection. Appropriate frequency. Multiple properties. Documentation.
Corrective Action
Failure investigation. Root cause analysis. Process correction. Verification testing. Documentation. Prevention measures.
Testing Best Practices
- •Thickness measurement using XRF provides fast non-destructive verification for production control
- •Adhesion testing validates coating bond strength catching preparation failures before shipping
- •Salt spray testing accelerates corrosion evaluation providing quality gate for protective coatings
- •Hardness and porosity testing verify functional properties beyond simple thickness measurement
- •Comprehensive quality programs combine testing with documentation and corrective action preventing defects